
Carbide Rotary Burr Type H
Technical Specifications
| Parameter | Specification |
|---|---|
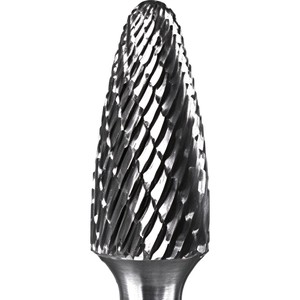
| Type / Shape | Type H — Flame-Shaped |
| Standard | ISO 7755 |
| Tooth Style | Double Cut (Cross-Cut) |
| Material | Ultra-fine grain tungsten carbide YG10X (WC + 10% Co) |
| Cutting Diameter × Cutting Length | 3×14 / 6×16 / 8×20 / 10×20 / 12×25 / 16×25 mm |
| Hardness | HRA 91.5 – 92.0 / HV ≥ 1400 |
| Grain Size | Ultra-fine (0.6 – 0.8 μm) |
| Shank Diameter | 6 mm (standard, suitable for 1/4" collet holders) |
| Recommended Speed | 10,000 – 40,000 RPM (depending on diameter) |
| Radial Runout | ≤ 0.03 mm |
| MOQ | 100 pcs per type / diameter |
Rotary Burr Technical Guide
Carbide rotary burrs (also called tungsten carbide burrs or die-grinder bits) are made of tungsten carbide (WC + Co) and run in high-speed electric or pneumatic die grinders and flexible-shaft machines. They remove material by the cutting edges on a spinning tool under feed pressure — ideal for deburring cast, forged and welded parts, chamfering and rounding edges, cleaning grooves and bores, and precision surface finishing. Typical operating speed: 6,000–50,000 RPM.
Standard Shapes — Type A to N (ISO 7755)
Rotary burrs follow the ISO 7755 shape-coding system. HARDVIK currently stocks Type A, B, C, E, F, G, H, L, M; the remaining shapes are available on request.
| Type | Shape | Description & Typical Use | Availability |
|---|---|---|---|
| A | Cylinder, flat top 圆柱形无顶刀 | Flat-end cylinder for flat-surface deburring, contour finishing and edge chamfering on straight surfaces. | In stock |
| B | Cylinder, with end cut 圆柱形带顶刀 | Cylinder whose end face also cuts — deburring and contouring including the front face. | In stock |
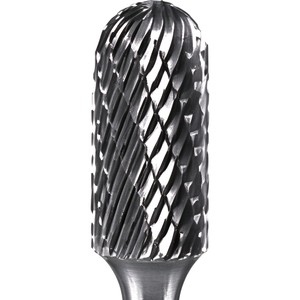
| C | Cylindrical ball-nose 球头圆柱形 | Rounded-end cylinder for fillets, rounded contours and curved profiles. | In stock |
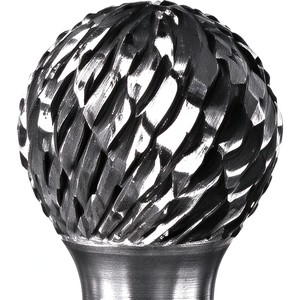
| D | Spherical / Ball 球形 | Full ball for rounding edges, concave radii and hollowing. | In stock |
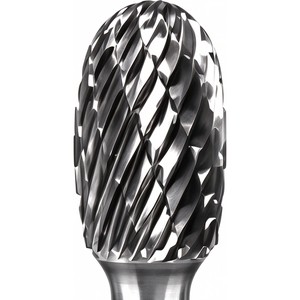
| E | Oval / Elliptical 椭圆形 | Oval profile for contouring and finishing curved surfaces. | In stock |
| F | Round / Arch (tree radius) 圆头弧形 | Rounded "tree" for rounding edges and fillets. | In stock |
| G | Pointed tree (radius tip) 尖头树形 | Tapered tree with a radiused tip for angled surfaces and hard-to-reach corners. | In stock |
| H | Flame / Tapered radius 火焰形 | Flame shape for rounding edges and contouring on curved profiles. | In stock |
| J | 60° cone 60°孔锥形 | 60° included-angle cone for chamfers, countersinks and V-grooves. | In stock |
| K | 90° cone 90°孔锥形 | 90° cone for deburring holes and chamfering. | In stock |
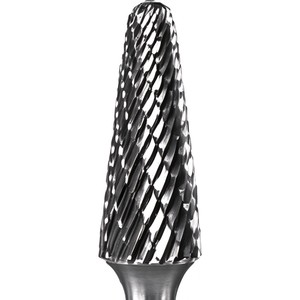
| L | Ball-nose cone 球头圆锥形 | Tapered with a rounded tip for rounded chamfers, contours and tight areas. | In stock |
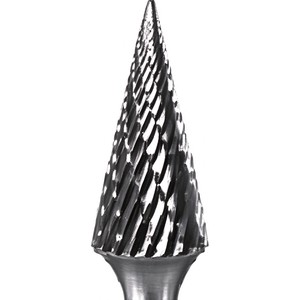
| M | Cone / Conical 圆锥形 | Straight cone for deburring holes, chamfering and V-cuts. | In stock |
| N | Inverted cone 倒锥形 | Reverse cone for internal chamfers, hole deburring and V-grooves. | In stock |
Tooth Style: Single Cut vs Double Cut
Single Cut 单齿
Flutes run in one direction. Aggressive stock removal on ferrous metals, with a coarser finish and more vibration. Best for rapid material removal on steel and cast iron.
Double Cut 双齿 / Cross-Cut — HARDVIK Standard
Crossed flutes produce smaller chips, less chatter and a smoother finish on both ferrous and non-ferrous metals. This is the default tooth style across the HARDVIK rotary-burr range.
Recommended Operating Speed
Smaller heads run faster; larger heads need lower RPM to stay safe. The table below is general guidance by head diameter — always follow the maximum RPM printed on the tool or the manufacturer's data sheet.
| Head Diameter | Reference Max Speed (RPM) |
|---|---|
| 3 mm | 30,000 – 50,000 |
| 6 mm | 20,000 – 35,000 |
| 8 mm | 15,000 – 28,000 |
| 10 mm | 12,000 – 22,000 |
| 12 mm | 10,000 – 18,000 |
| 16 mm | 6,000 – 14,000 |
Safety note: keep the exposed shank length at ≤ 13 mm for standard tools. Extended-shank burrs must run at a lower, safer speed.
Why Carbide Rotary Burrs
- Wide material range — cast iron, cast steel, carbon steel, alloy steel, stainless steel, copper, aluminium, and even non-metals such as marble, jade and bone.
- Dust-free & safe — replaces bonded abrasive wheels, eliminating the dust and breakage risk of small mounted stones.
- High efficiency — material removal is tens of times faster than manual filing and several times faster than small abrasive wheels.
- Long service life — far outlasts high-speed-steel tools and lasts hundreds of times longer than bonded abrasive wheels.
- Superior finish — produces a smooth, high-quality surface that needs less secondary work.
- Easy & economical — simple to master, reliable in use, and lowers the overall cost per part.
Product Description
The HARDVIK Carbide Rotary Burr Type H (Flame-Shaped) is a precision double-cut tungsten carbide burr for high-performance material removal, deburring and surface finishing. Ground to ISO 7755 from ultra-fine grain YG10X carbide and brazed to a 6 mm steel shank, it delivers fast, smooth stock removal with a long service life.

Key Features
- Double Cut (Cross-Cut) Tooth Design — smoother finishes and better chip control than single-cut burs, with reduced clogging on ferrous and non-ferrous metals.
- Premium Tungsten Carbide (YG10X) — ultra-fine grain WC with 10% cobalt binder for exceptional hardness and wear resistance.
- Hardness HRA 91–92 (HV ≥ 1400) — long service life; the cutting edge stays sharp even under high-temperature conditions.
- 6 mm Standard Shank — fits all standard pneumatic / electric die grinders, flexible shaft machines and CNC spindles.
- Precision Ground to ISO 7755 — consistent dimensions and runout ≤ 0.03 mm for vibration-free operation.
- Wide Material Compatibility — cast iron, carbon steel, alloy steel, stainless steel, hardened steel (≤ HRC65), copper, brass, aluminum and plastics.
Applications
- Curved and complex contours
- Blending concave-to-convex transitions
- Removing sharp edges, burrs and flash from machined, cast, forged or stamped parts
- Mold & die cavity and core finishing
- Cleaning intersecting drilled holes, hydraulic ports and pneumatic valve bodies
Production Process
- Powder preparation — ultra-fine WC–10%Co mixture
- Pressing & sintering of the burr head
- Brazing the carbide head to the steel shank
- CNC fluting and precision grinding of the cutting profile
- 100% inspection — dimensions, hardness and runout
- Packing and shipping
Machining Guide
Use with die grinders, flexible shaft machines or CNC spindles at 6,000–50,000 RPM (lower speed for larger diameters; standard-length tools expose up to 13 mm of shank). Keep the tool moving with light pressure to avoid glazing and get the best finish.

Ordering Information
Standard cutting diameters Ø3–16 mm with 6 mm shank. MOQ: 100 pcs per type/diameter. Custom sizes, coatings (TiAlN/TiSiN) and packaging available on request. For bulk pricing and technical consultation, contact our sales team via WhatsApp or email.
SKU: HV-RB-H
Our Advantages
Payment Methods
Payment Terms
Standard: Default 100% T/T advance payment.
Premium customers: Buyers with good credit and repeat order history may pay a minimum 50% deposit; the remaining 50% balance must be settled before packaging and labeling.
Channels: We recommend XTransfer (supports all global currencies) or Alibaba Trade Assurance orders.
Currency & Trade Terms
USD settlement (recommended): We handle export customs clearance ourselves, fully compliant with Chinese laws and regulations.
RMB settlement: Only available under EXW or FOB terms; export customs clearance is the buyer's responsibility.
Alibaba Trade Assurance
Orders can be placed through Alibaba Trade Assurance order links.
Note: The 3% Trade Assurance service fee is borne by the buyer.
Certifications
Certified Quality
ISO9001 certified, verified by SGS video inspection, and recognized as an Alibaba Verified Supplier.
Brand & R&D
Owner of the proprietary "HARDVIK" brand, backed by multiple invention and utility model patents.
Global Trade
Fully licensed for independent import/export operations, with support for multi-currency local payments worldwide.

Frequently Asked Questions
What is your MOQ (Minimum Order Quantity)?
What is the delivery time?
If blanks are not in stock, production takes 25-45 days.
If customization by drawing is required, molds must be made — this typically takes 30-60 days.
For additional customization:
- Coating: 3-10 days
- Repackaging (changing boxes): 1-2 days
- Repackaging with new labels: 1-2 days
- Custom label production: 3-7 days, plus 1-3 days for manual application
Sample orders: 3-7 days. Expedited service is available for large orders willing to pay a rush fee.
Can you send samples before placing a bulk order?
What payment methods do you accept?
We recommend USD payments. For RMB payments, we only support EXW and FOB shipping terms — customs clearance is the buyer's responsibility. For USD payments, we handle customs export ourselves, which complies better with Chinese law. We welcome USD payment arrangements.
We primarily use XTransfer for payment collection, which supports all global currencies.
Do you provide OEM/ODM services?
1. Replica Manufacturing — Send us a sample or photo of any carbide insert; we can replicate it with exact dimensions, geometry, and coating.
2. Price-Based Customization — Tell us your target price; we engineer the best possible product within your budget.
3. Custom Packaging & Branding — Custom boxes with your brand logo, labels, and barcodes. Full private-label service for distributors.
4. Free Coating & Color Options — 8+ coating colors at no extra cost. Box color customization also free of charge.
Have more questions? Send us a message.
Send Message